


Forklift Work Light with Amber Signal: Lighting and Safety Combined
In modern warehouses and logistics centers, visibility and safety are two crucial factors that determine efficiency and accident prevention. The forklift work light with an integrated amber warning function is an innovative solution that addresses both needs at once. Engineered for industrial performance, this LED light offers powerful white illumination for work tasks and bright amber signaling for warning and direction indication. Let’s take a deeper look at how this versatile lighting system enhances workplace safety and productivity.
1. Dual Function: Work Illumination + Directional Indication
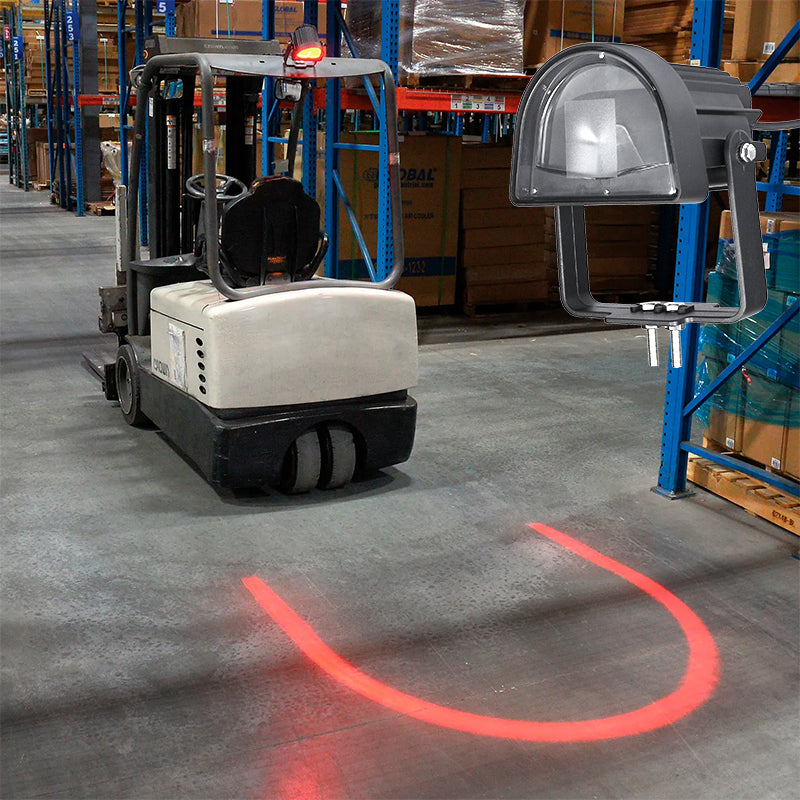
This forklift light integrates 5 pieces of 1W white LEDs dedicated to work illumination and 3 pieces of 0.5W amber LEDs for direction indication or signal warning.
-
The white LEDs produce up to 480 lumens (WK: 480LM) of clear, bright light—perfect for lighting up loading zones, aisles, or workspaces in dim environments.
-
The amber LEDs generate around 100 lumens (DI: 100LM) of warning light, serving as a visible signal to alert pedestrians or nearby operators of forklift movement.
This dual-color system improves visibility not just for the operator but for everyone in the surrounding area, effectively minimizing collision risks and operational hazards.
2. High-Quality LED Performance
Equipped with high-power Epistar LEDs, the light provides consistent brightness and reliable color output even in long-hour operation. These LEDs are energy-efficient, generate minimal heat, and ensure a long service life exceeding 50,000 hours.
The white light enhances clarity during warehouse operations, while the amber beam serves as a visual cue to prevent workplace accidents — especially in busy or low-visibility environments.
3. Robust Construction for Harsh Conditions
Industrial environments can be tough, and forklift lights must withstand constant vibration, dust, and temperature variation. This light is built with a die-cast aluminum housing that provides excellent heat dissipation and corrosion resistance. The PC lens cover ensures strong protection against impact and scratches, while the stainless steel mounting bracket keeps the fixture stable and secure under continuous movement.
The unit also supports a wide operating voltage range of DC10–80V, compatible with most types of forklifts, loaders, and material handling vehicles.
4. Reliable in Extreme Environments
Whether operating in freezing warehouses or hot outdoor conditions, this work light performs consistently across a -40°C to +80°C temperature range. It’s IP67-rated, meaning it is completely dustproof and resistant to water immersion. Rain, snow, or heavy dust will not interfere with its function — a critical feature for logistics and construction environments that operate under diverse weather conditions.
5. Safety and Compliance
This forklift light meets CE certification standards and includes reverse polarity protection to prevent damage from incorrect wiring during installation. These features ensure the product’s reliability and safety for industrial use, aligning with global compliance requirements.
6. Versatile Beam Options and Applications
The light adopts an optional flood beam design, which spreads light evenly over a wide area — ideal for illuminating work zones, shelves, and pathways.
Common application scenarios include:
-
Forklifts and reach trucks in warehouses
-
Construction machinery and loaders
-
Agricultural equipment and service vehicles
-
Dockyards, loading bays, and logistics centers
By combining white work illumination with amber directional light, this solution is adaptable to both operational and safety purposes.
7. Long-Term Efficiency and Cost Savings
Beyond brightness and safety, the long lifespan and low energy consumption of the LEDs significantly reduce maintenance costs. With an average working time of over 50,000 hours, operators can rely on continuous lighting without frequent replacement. The low power draw also minimizes energy consumption, contributing to a more sustainable operation.
8. Simple Installation and Maintenance
Installation is straightforward thanks to the adjustable stainless-steel bracket, which allows flexible mounting angles to direct light exactly where needed. The compact oval shape also makes it easy to fit on different parts of a forklift—front, rear, or side—depending on the lighting requirement.
Maintenance is minimal: occasional cleaning of the PC cover and checking of the mounting bolts ensure optimal performance over time.
9. Why Choose a Dual-Color Forklift Light
Traditional forklift lights often provide only illumination. However, in modern safety-oriented warehouses, it’s equally important to communicate motion and presence through visual cues. The amber light warns pedestrians when the forklift is approaching or reversing, effectively reducing accident risks. Combining both illumination and signaling functions into one compact unit simplifies installation and enhances operational awareness.
10. Conclusion: A Complete Lighting Solution for Industrial Safety
This dual-function forklift light is more than just a lighting tool—it’s a safety system designed to make industrial operations safer, clearer, and more efficient. With its combination of 480-lumen white work light and amber directional indicator, operators can confidently handle tasks while ensuring others nearby stay aware of vehicle movements. The rugged design, IP67 protection, and long lifespan make it a dependable choice for any professional working environment.